Offshore changes a cylinder specification in ways that are mostly invisible in the price until something fails. The force requirement barely moves; what moves is everything around it.
Corrosion class is a specification, not a paint code
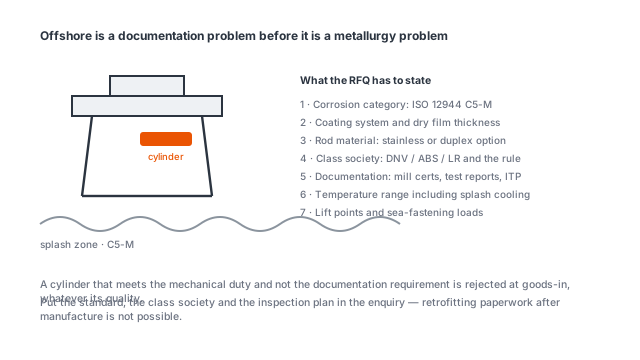
ISO 12944 splits atmospheric corrosivity from C1 to CX. An offshore platform topside is C5-M, and anything in the splash zone needs an additional system, because the surface is alternately wetted, dried and hit by spray carrying abrasive sand.
The practical differences from a standard cylinder:
- Surface preparation. Sa 2.5 shot blast, not a wire brush. Coating over mill scale fails within a season offshore.
- Coating thickness. 320 µm total dry film in a multi-coat system for C5-M, against 80 to 120 µm for a normal industrial cylinder.
- Fasteners and fittings. Stainless throughout. A zinc-plated bolt disappears in a marine atmosphere and takes the paint around it with it.
- Rod. 316 stainless or duplex, with hard chrome or a ceramic coating for wear. A chrome-plated carbon rod is acceptable only where a boot prevents any salt reaching the surface, which is rarely true on deck.
The rod is the part that decides most offshore cylinder life, because it is the only surface that moves in and out of the protected envelope several times a minute. A 20 µm chrome on a carbon rod will develop pits in a salt atmosphere at the point where the wiper rests, and once a pit forms the seal cuts within weeks.
Seals and the service interval
The second offshore constraint is that maintenance windows are set by the vessel or the platform, not by the cylinder. A cylinder that would be resealed on a tipper every two years has to survive the same interval with no access at all.
That pushes the seal package toward:
- NBR replaced by FKM or HNBR for temperature and fluid tolerance, particularly where the hydraulic fluid is a water-based or biodegradable type.
- A double wiper with a drainage gap, so salt crystals pushed back along the rod are trapped rather than driven into the seal.
- A boot wherever the rod is exposed, with a drain at the low point. A boot that fills with water is worse than no boot.
- A breather on the rod side rather than a sealed gland, so that pressure changes from temperature cycling do not pump seawater past the wiper.
Certification is part of the RFQ
Classification requirements come from the class society, not from the cylinder supplier, and the scope varies with whether the cylinder is safety-critical. A deck crane luffing cylinder on a liftboat and a hatch cover cylinder on a barge are both “offshore” and are not specified the same way.
What the RFQ needs to state: the class society, the design code, whether design review is required, whether pressure testing must be witnessed, and the material traceability standard. Leaving those out is how a cylinder arrives certified to the wrong scope.
Where the standard range fits
Deck functions that need long stroke at moderate force fit the HSG range: 430 to 3,500 mm of stroke at 20 MPa, bore and rod from 50/28 to 200/140 mm across 7 models. A davit or a hatch cover actuator is a good match once the material and coating specification is layered on top.
Where no engine or three-phase supply is available, the DC hydraulic power unit covers 12 V or 24 V, 0.75 to 8 cc/rev, 3 to 25 L/min, 3 to 16 L reservoirs and 50 to 250 bar. Marine installations normally add an IP-rated enclosure and tinned cable, neither of which is standard.
What to send
Exposure zone, class society and code, fluid type, service interval and whether the cylinder is in a hazardous area. Those five answers determine coating system, rod material, seal package and documentation scope, and they are the difference between a quote and a specification argument six months later.